
A custom activewear buyer should approve more than the appearance of a pre-production sample. The approval file should confirm the controlled tech pack, fit and measurements, production fabric and color, construction, branding, labels, packaging, testing requirements, and the exact conditions that release bulk production. Each item needs a clear status, approver, date, and reference. If a requirement is still open, the order is not ready for an unconditional production release.
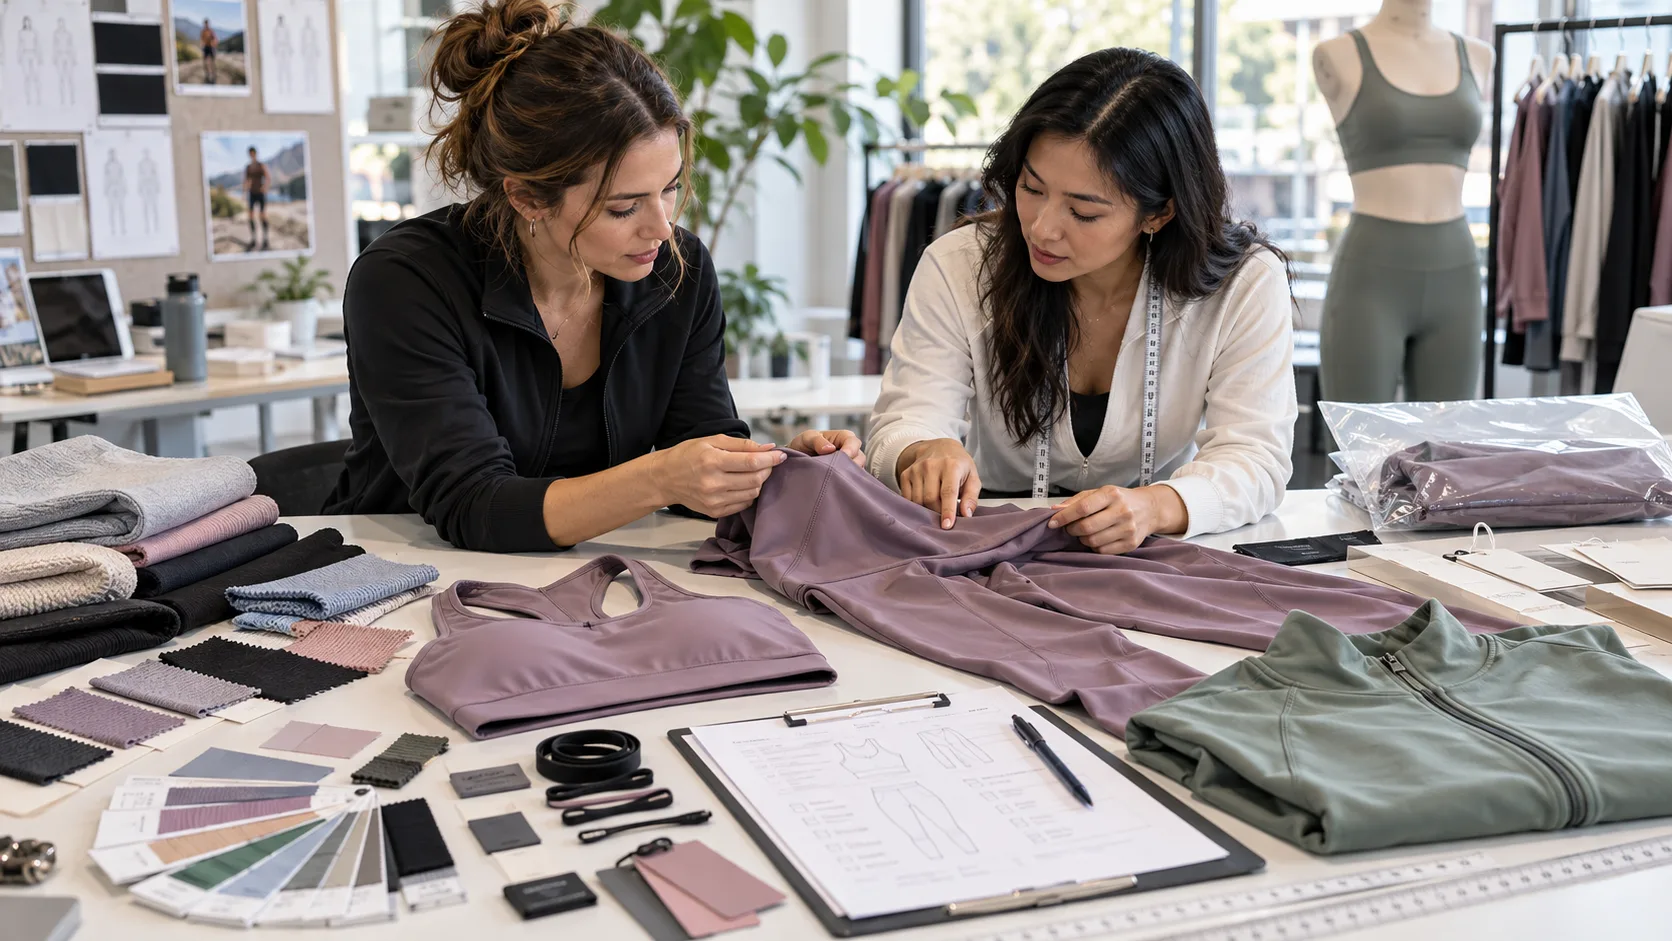
Start With the Purpose of the Pre-Production Sample
PP Sample Approval Is a Production Release Decision
| Stage | Required control |
| Approved specification | Controlled tech pack, BOM, size chart, artwork and packaging |
| Production-intent PP sample | Representative materials, fit, trims and workmanship |
| Verification evidence | Measurement, fabric/color, performance and inspection records |
| Open-issue closure | Owner, deadline and accepted corrective evidence |
| Authorized release | GO / CONDITIONAL GO / HOLD with operation-specific scope |
The pre-production sample, or PP sample, is the final physical reference before bulk manufacturing. It should represent the approved materials, trims, workmanship, colors, artwork, labels, and packaging closely enough to act as a production benchmark.
Do not confuse it with an earlier prototype or fit sample. A prototype helps resolve design direction. A fit sample checks shape and measurements. The PP sample confirms that the finalized specification can be reproduced with production-intent inputs. If final fabric, elastic, logo application, or labels are unavailable, record the substitution and require approval of the real component before its bulk use.
PP Sample vs. Other Sample Types
Prototype: design feasibility. Fit sample: pattern and movement. Size-set sample: grading across sizes. Sales sample: commercial presentation. PP sample: production-intent approval. TOP (top-of-production) sample: optional verification of actual bulk output where the buyer requires it. A TOP sample does not replace PP approval.
A PP sample is not approved simply because it looks correct. The physical sample, controlled documents, production inputs and evidence must align.
Put These Eight Approval Blocks on the Checklist
Eight Approval Blocks — Quick Reference
| Block | Evidence | Principal risk |
| Document control | Approved revision register | Wrong document |
| Fit & grading | POM report / size-set review | Fit variation |
| Fabric & color | Approved swatch, lab dip, tests | Material mismatch |
| Construction | Workmanship standard | Sewing inconsistency |
| Branding & trims | Artwork and BOM approvals | Placement error |
| Labels & packing | SKU/barcode master | Wrong identification |
| Quality plan | Tests and inspection plan | Undefined acceptance |
| Production readiness | Material allocation and release | Premature bulk start |
1. Document Control and Style Identity
Begin with one source of truth. Record the style number, season, colorway, size, purchase order, sample round, tech-pack revision, and sample date. Confirm that the bill of materials, measurement chart, artwork files, and packing instructions carry matching revision numbers.
Withdraw obsolete documents. A sample approved against one measurement chart while the sewing team uses another is not an approved standard. The sign-off sheet should identify the buyer approver and the supplier contact responsible for transferring the release to production.
Master Revision Register
Keep one approved production package with a document ID, individual revision, approval status, date and owner for each tech pack, measurement chart, grading rule, BOM, fabric specification, artwork, label and packing file. Different documents need not share the same revision number; they must be explicitly linked to the same current approved package.
Mark obsolete versions clearly and withdraw them from sample room, cutting, sewing, decoration, quality and packing teams.
2. Fit, Measurements, and Grading
Measure the PP sample using the method stated in the tech pack. Check every defined point of measurement against its specification and tolerance, then test fit on the intended body or fit model where appropriate.
Activewear needs review in movement, not only on a table. Check whether armholes, waistbands, crotch depth, leg openings, and compression zones remain comfortable and stable through the product’s intended range of motion. Confirm the approved base size and grading rules. If only one size is reviewed, identify which size-set evidence is still required before all sizes enter production.
Fit and Size-Set Approval Rules
The figures above illustrate record format only, not universal tolerances. Use the buyer-defined POM measurement method. Base-size fit approval does not automatically approve grading across the full size range.
Choose movement checks by garment: leggings—squat/lunge, opacity, waistband and gusset; sports bras—arm raise, band and strap; running shorts—running, mobility and ride-up; training tops—reach and twist; compression garments—intended movement, pressure and recovery. Record size, fabric, fit model, issue and disposition.
Illustrative Measurement Approval Matrix
| POM | Spec | Tolerance | Actual | Result |
| Waist | 68 cm | ±1 cm | 68.5 cm | Pass |
| Hip | 88 cm | ±1 cm | 89.5 cm | Fail |
| Inseam | 65 cm | ±1 cm | 65 cm | Pass |
| Leg opening | 20 cm | ±0.5 cm | 20 cm | Pass |
3. Fabric, Color, and Material Performance
Confirm fiber composition, knit construction, target weight, finish, hand feel, stretch, recovery, opacity, and color. Compare the sample with the approved fabric swatch and lab dip under the agreed viewing conditions. For matching sets or mixed materials, review adjacent panels together rather than approving each component in isolation.
The buyer should also specify the tests required for the actual claim and use case. Depending on the product, this may include dimensional stability after washing, colorfastness, pilling, seam behavior, stretch recovery, or opacity under intended stretch. Test methods and acceptance criteria must be agreed rather than inferred from a marketing phrase. Harvest SPF’s custom sportswear programs include material selection and sample development, giving buyers a practical point at which to lock these decisions.
Fabric-to-Garment Compatibility and Approval Evidence
Approve the complete fabric system: composition, GSM, knit construction, stretch, extension force, recovery, finishing and end-use fit. Two fabrics with similar nominal composition and GSM may perform differently. A fabric substitution may require renewed fit and performance approval.
Attach evidence by property: supplier material specification; GSM and stretch/recovery results where required; approved swatch and lab dip; buyer-defined stretched-opacity check; wash dimensional stability, pilling and claim-related tests with agreed methods and limits.
Colorway approval can be risk-based: a common construction PP sample may support several colors, but each colorway still needs relevant shade, artwork and trim approvals; significant changes may need another PP validation.
4. Construction and Workmanship
Inspect the garment inside and out. Verify seam type, stitch density where specified, thread, reinforcement, bartacks, elastic insertion, pocket construction, zipper operation, and edge finishing. Look for puckering, skipped stitches, twisting, uneven tension, raw edges, or uncomfortable bulk at high-friction areas.
Compare construction with the callouts in the tech pack. If a production method changes during development, update the specification before approval. A verbal acceptance of the sample should not leave the factory with an outdated construction drawing.
Activewear Critical-to-Quality (CTQ) Points
Leggings: squat opacity, waistband stability and inseam/gusset. Sports bras: underband, straps, support and seam comfort. Running shorts: mobility, pockets and waistband. Compression garments: measurements, extension force, recovery and intended pressure. Verify flatlock/overlock/coverstitch, seam stretch, reinforcement, elastic insertion and heat-transfer durability as applicable; no single seam type is universally best.
5. Branding, Trims, and Placement
Check the logo method, size, color, position, orientation, and adhesion or stitch quality. Review prints and heat transfers on the production fabric because stretch, surface texture, and heat can change their appearance. Confirm drawcords, elastic, zippers, cups, pads, hooks, and other trims against the bill of materials.
Record placement measurements from fixed garment reference points. Photos help communicate the approved appearance, but they should supplement—not replace—dimensioned artwork and placement instructions. For a complete view of available activewear styles and constructions, buyers can review Harvest SPF’s Fitness & Yoga range during specification development.
Artwork and Trim Approval Record
For each logo/trim, record application method, approved dimensions, placement from fixed POM, color, artwork revision, approved component and any buyer-required stretch/wash validation. Photos supplement dimensioned artwork; they do not replace it.
6. Labels, Packaging, and SKU Accuracy
Approve care and content labels, brand labels, size labels, hangtags, barcode data, polybags, folding, carton assortment, and carton marks. Verify that the physical garment, label, barcode, bag, and carton all identify the same style, color, size, and destination.
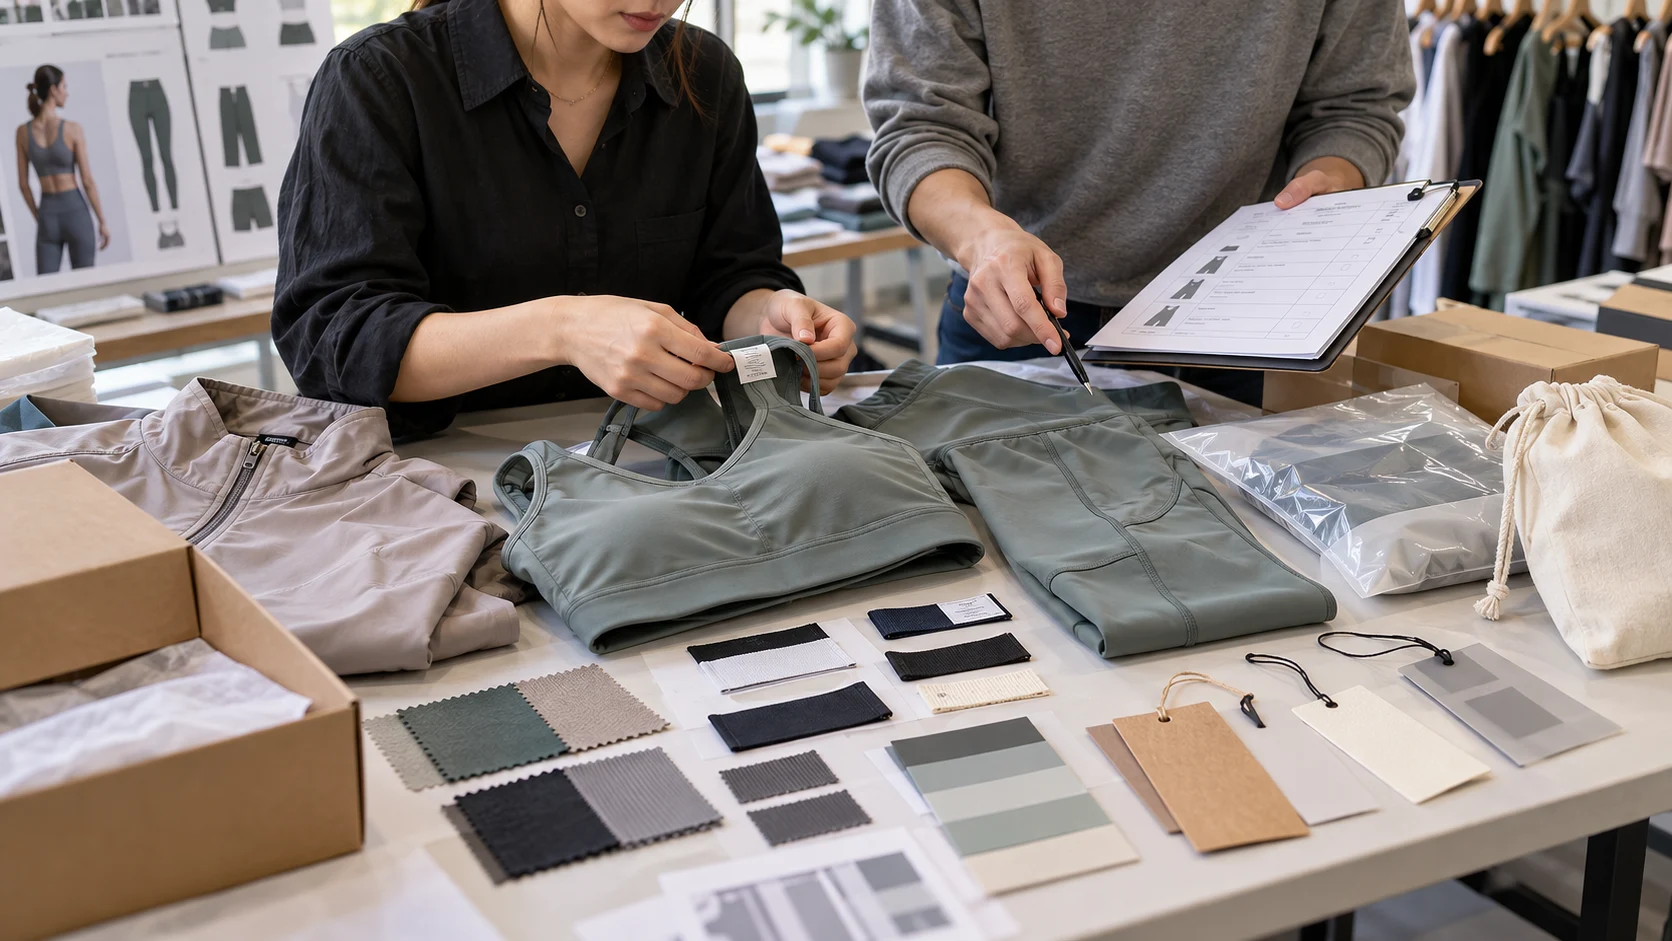
Compliance wording depends on the product and destination market, so the buyer should provide approved market-specific artwork or obtain qualified advice. Scan each barcode and compare the decoded value with the SKU master; a successful scan alone does not prove that the code belongs to the correct SKU. Harvest SPF’s ODM/OEM process places client proofing, packaging and labels, mass production, quality inspection, packing, and shipping in a defined sequence.
One SKU Identity From Garment to Carton
Confirm style + color + size + destination market across garment label → hangtag/barcode → polybag → carton label → packing list. A successful scan alone is insufficient: verify scannability, decoded value, SKU master and correct packaging level.
7. Quality Plan and Release Evidence
Turn subjective expectations into inspection criteria. Define measurement tolerances, defect categories, sampling plan, required tests, and who can accept or reject nonconforming goods. State whether inline, final, buyer-appointed, or third-party inspection is required.
The approval pack should contain the signed PP sample record, approved tech pack, bill of materials, color and artwork approvals, test requirements, and packaging master. Keep a sealed reference sample with traceable identification when the program permits. A related Harvest SPF guide on seasonal color approval explains why an approved lab dip still needs a controlled link to bulk dye lots.
PP Approval Evidence Package and Inspection Boundary
File the signed PP approval, identified/sealed reference where practical, current tech pack and BOM, measurement/size-set evidence, fabric/color approvals, artwork/trims, required test reports, packaging master, issue closure and authorized release.
PP approval defines the intended production standard; it does not replace inline inspection, final inspection or shipment release. Agree defect classifications (critical/major/minor), sampling method, acceptance criteria and authority before bulk; no single AQL level applies to every buyer or product.
8. Production Readiness and Change Control
Before signing, confirm that approved materials are allocated, the order quantities and SKU breakdown are final, capacity conditions are understood, and open issues have owners and due dates. Use only three release outcomes:
Pre-Bulk Readiness Matrix
| Area | Status | Evidence |
| Tech pack / fit | Ready / Open | Approved revision / fit report |
| Fabric / color | Ready / Open | Material approval / shade record |
| Artwork / labels | Ready / Open | Approved artwork / label files |
| Packaging / SKU | Ready / Open | Packing master / barcode verification |
| Quality | Ready / Open | Test and inspection plan |
| Materials / capacity | Ready / Open | Allocation / schedule |
| Open issues | Closed / Open | Accepted action log |
- Approved: bulk production may proceed to the identified revision.
- Approved with conditions: production may proceed only after listed evidence is accepted.
- Rejected or hold: bulk production must not start.
Define how changes after approval will be controlled. Any change to fabric, color, construction, artwork, trim, label, or packing should trigger documented review and, when material, a new sample or approval. The release should never authorize the supplier to make unspecified “equivalent” substitutions.
GO / CONDITIONAL GO / HOLD — Operation-Specific Release
GO: all critical approvals closed; identified bulk operations may proceed against the released revision.
CONDITIONAL GO: list precisely which operations are permitted, which remain blocked, who owns each condition and what evidence closes it. An open issue must not be carried into an affected production step.
HOLD: do not begin affected bulk operations until the critical fit, material, color, construction, compliance or quality issue is resolved.
PP approval and production readiness are separate checks. After approval, any proposed material, fit, artwork, trim or packaging substitution follows: change request → technical impact → cost/MOQ/lead-time review → targeted sample/test if needed → buyer approval → updated documents → revised release.
Use One Consolidated Approval Record
Consolidated PP Approval & Sign-Off Sheet (Example)
| Item | Result | Issue / action | Owner | Status |
| Tech pack | Pass | — | Technical | Closed |
| Fit | Fail | Adjust waist | Pattern | Open |
| Fabric | Pass | — | Material | Closed |
| Logo | Conditional | Confirm wash test | Supplier | Pending |
| Packaging | Pass | — | Merchandising | Closed |
Design, merchandising, technical, quality, and logistics teams may all comment, but the factory should receive one reconciled response. A useful approval record includes the requirement, reference, result, comment, owner, due date, status, approver, and date. Attach marked photos for visible issues and quote the current document revision in every response.
Set a deadline for each approval round. Conflicting emails and unnumbered attachments create more risk than a carefully documented hold. Harvest SPF describes prototype sampling followed by client proofing and a pre-production sample before bulk manufacturing; buyers should use those stages as formal decision gates rather than informal review rounds.
Final Sign-Off and Responsibility
Record buyer authorized approver, supplier production representative, style/color/size scope, current revision, date and release status. Typical reviewers: technical design—fit; materials—fabric; design—color/artwork; QA—testing/quality; compliance—market labels; merchandising/logistics—packaging. Assign one final release authority, even when multiple teams review.
Conclusion
How Harvest SPF Supports Activewear PP Sample Approval
Harvest SPF can coordinate technical specification review, fabric/color and trim development, prototype/fit/PP sampling, construction and branding checks, packaging/SKU confirmation, buyer-required testing coordination and bulk specification handoff, subject to the actual project scope.
The objective is a traceable link from the buyer-approved PP sample to the documents, materials and controls used for bulk production.
A strong custom activewear pre-production approval checklist connects the physical sample to controlled specifications and a documented production release. It covers fit, fabric, color, construction, branding, labels, packaging, quality criteria, and change control. The most important rule is simple: every open point must become an owned action—not an assumption carried into bulk production.
FAQs
Can bulk production start with conditional PP approval?
Only if the conditions are explicit, low risk, assigned, and verified before the affected operation begins. Any unresolved issue that could change fit, material, color, construction, branding, or compliance should remain on hold.
Who should sign the pre-production approval?
The buyer should name an authorized approver, often from product development, technical design, or quality. Supplier acceptance should also identify who is responsible for transferring the approved revision into production.
Can bulk start before PP approval?
Affected production operations should remain blocked unless the buyer grants explicit, documented, risk-defined authorization.
Does PP approval guarantee bulk quality?
No. Process control, agreed inspection and shipment-release criteria remain necessary.
Does every colorway need a separate PP sample?
Not always; define risk-based PP coverage and separately approve each relevant color/component.
What if the fabric changes after PP approval?
Review fit, stretch/recovery, color, performance and construction; retest or resample where needed.
What documents should accompany PP approval?
Current tech pack/BOM, measurements, material and color approvals, artwork, test evidence, packaging master, signed issue closure and release.
Start Your Custom Activewear Project With Harvest SPF
Get a Custom Activewear PP Sample & Bulk Readiness Review
Send Harvest SPF the style/tech pack, sample stage, fabric specification, size range, colorways, branding and trim details, buyer-required tests, packaging, order quantity, destination market and delivery date. The team can discuss missing approval items, sampling needs, material/color risks, quality criteria, open issues and bulk readiness within the agreed service scope.
Review My Activewear PP Sample